


PVC SG5 Resin: What Its K-Value Means for Pipes, Profiles, and Fittings
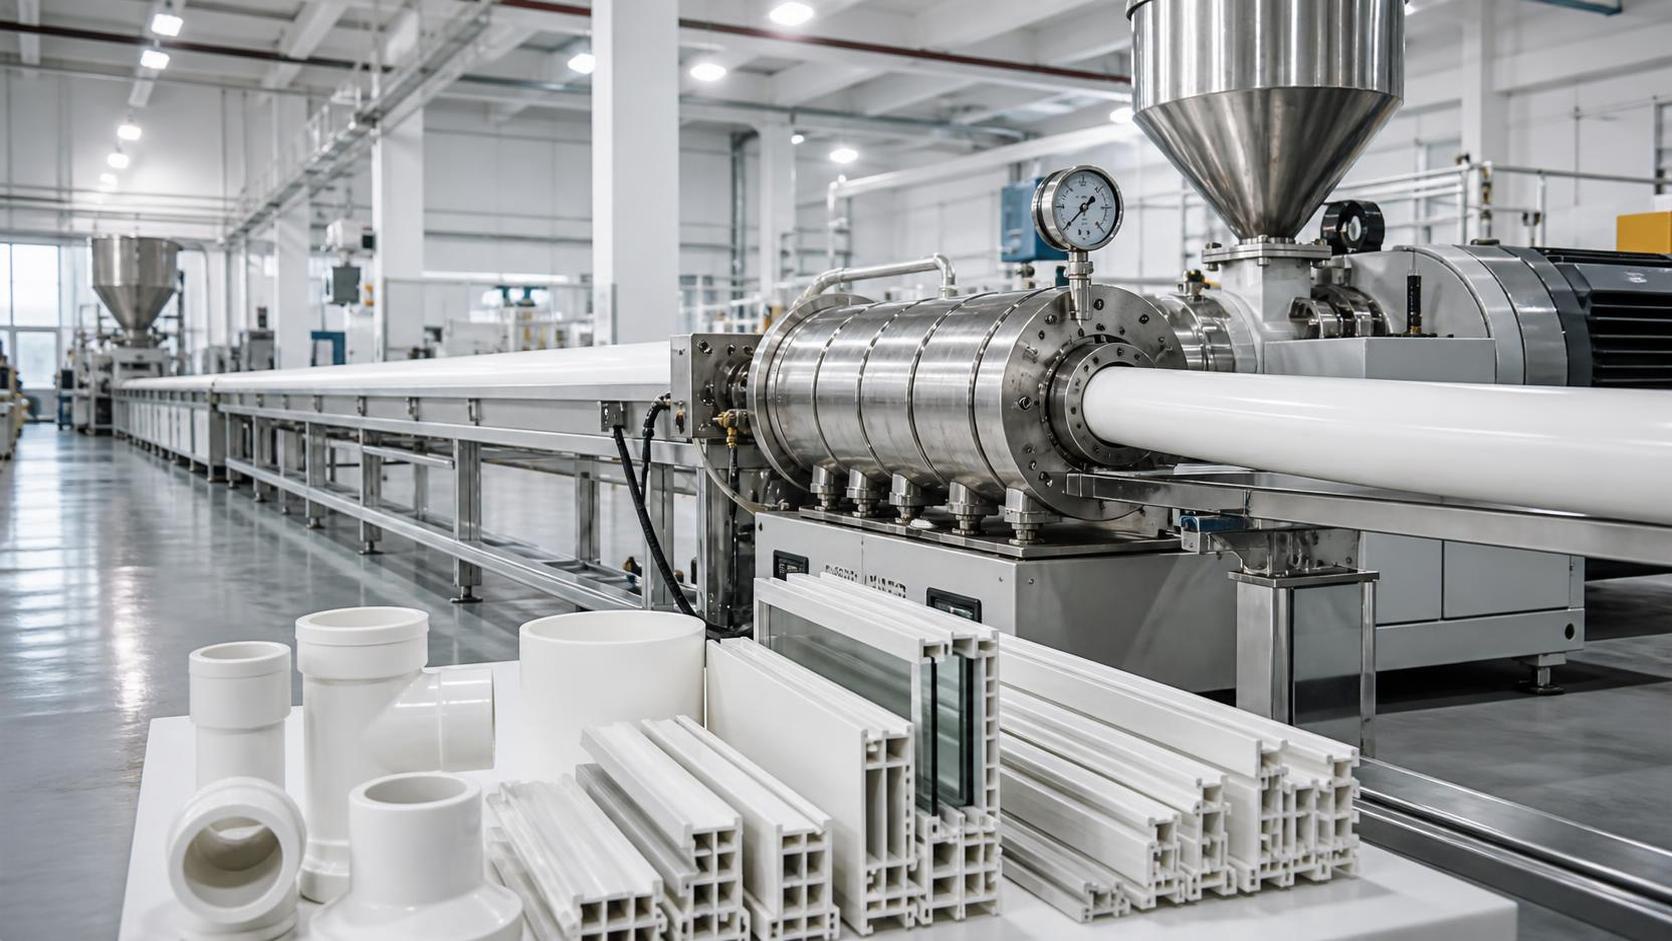
A pipe extrusion line can appear stable for most of a shift and then begin to show small but costly warning signs: die pressure drifts upward, the surface loses its clean finish, pipe stiffness feels inconsistent, or fittings made from the same compound show uneven fusion. In many plants, the first reaction is to change lubricant level, barrel temperature, or screw speed. Those adjustments may help temporarily, but they do not always address the source of the problem.
A common issue is that the resin grade has been treated as a generic PVC material rather than as a material with a defined molecular-weight range and processing character. For rigid pipes, profiles, and injection-molded fittings, the K-value is one of the practical indicators that deserves attention before a formulation is changed. When PVC SG5 resin is selected, understood, and handled correctly, it gives a workable balance between processing behavior and final mechanical performance. When it is substituted without review, even a familiar formula can become difficult to control.
The production question behind “SG5”
Suspension PVC grades are commonly identified by K-value categories. The K-value is linked to the viscosity behavior of PVC in solution and is used as an indirect indicator of molecular weight. A higher K-value generally corresponds to longer polymer chains and higher molecular weight. That change affects melt resistance, gelation behavior, mechanical properties, and the amount of energy needed during processing.
PVC SG5 is generally positioned as a medium K-value suspension resin used widely in rigid PVC applications. It is often considered suitable for pipes, window and construction profiles, conduit, sheets, and many fitting formulations. However, “suitable” does not mean that every SG5 lot, every compound design, and every processing setup will behave identically. Resin properties, additive package, moisture condition, equipment design, and the intended product all interact.
For day-to-day material decisions, the useful question is not simply whether a bag says SG5. The better question is: does the resin’s molecular-weight level and physical condition match the balance of stiffness, fusion window, output, and surface quality required by the product?
Why the K-value becomes visible on the line
In rigid PVC, processing is not just melting in the usual thermoplastic sense. PVC particles must be heated, mixed, compacted, and fused into a uniform melt while avoiding thermal damage. Molecular weight influences how the resin responds during this process.
A resin with relatively higher molecular weight can provide stronger melt resistance and may support certain mechanical requirements. At the same time, it can require more shear, heat input, or residence control to reach the desired fusion condition. If the equipment or formulation does not supply enough effective processing energy, the compound may show incomplete fusion, roughness, weak appearance, or poor weld-line behavior in molded parts.
At the other end, a lower molecular-weight resin may process more easily but can change melt strength and may affect properties that matter in pressure-bearing or load-bearing applications. The practical aim is not to pursue the highest or lowest K-value. It is to work within the grade range that the product design and process window can support.
That is why a change in resin source can be noticed even when the nominal label remains similar. A different particle structure, bulk density, volatile content, or lot-to-lot K-value distribution can alter material flow and fusion timing. If the line team responds only by increasing temperature, the result can be misleading: the surface may improve briefly while thermal stability becomes less forgiving.
A familiar troubleshooting path: pressure rises while the pipe surface gets worse
One of the more confusing production situations occurs when extrusion pressure rises gradually, output becomes less steady, and the pipe surface turns dull or slightly uneven. This may happen after a raw-material delivery change, after a formulation adjustment, or without an obvious event. It is tempting to blame the die immediately, especially when the die has been running for a long period.
Before dismantling equipment, separate the possible causes. A structured review usually saves time because several different issues can create similar symptoms.
Start with the material identity
Confirm the resin grade, lot identification, storage status, and receiving records. Do not rely only on informal descriptions such as “same PVC” or “standard pipe resin.” Review the supplier’s technical information for K-value range, apparent bulk density, volatile matter, particle characteristics, and any stated processing guidance. For PVC SG5, these details help explain whether the resin should be expected to behave like the material used during earlier production runs.
If retained samples are available, compare the current lot with a previous stable lot under the same test methods. The purpose is not to declare one lot good or bad based on a single value. The purpose is to identify meaningful differences that might shift dry blending, plastication, or extrusion response.
Then look at dry blend condition
Rigid PVC processing problems often begin before material reaches the extruder. Poor additive distribution, incomplete absorption of processing aids or lubricants, excessive blend temperature, and inconsistent cooling can all change fusion behavior. A resin with a different bulk density may occupy the mixer differently and alter the way additives distribute through the powder.
Check whether the hot-mix discharge condition and cold-mix cooling condition are consistent with the established formulation practice. Inspect powder flow rather than assuming that a free-flowing blend is automatically well prepared. Excessive agglomerates, abnormal dust generation, or a powder temperature that remains elevated can be early signals that the blend should be reviewed before extrusion settings are changed.
Compare fusion indicators, not only final appearance
Appearance is important, but it is a late indicator. When available, use the normal internal methods for monitoring fusion and thermal behavior. These may include torque behavior during mixing, fusion-related laboratory checks, gelation assessment, or comparison of extruder load and melt pressure trends. The exact test method depends on the facility, but the principle remains the same: determine whether the compound is under-fused, over-sheared, or simply responding to a different rheological balance.
If pressure is rising while the melt quality appears inconsistent, avoid making several major changes at once. Adjusting screw speed, all barrel zones, die temperature, and lubricant dosage together removes the ability to identify the real cause. Make one controlled change, document the response, and compare it with a defined baseline.
Matching SG5 resin to pipes, profiles, and fittings
The same resin grade can serve different applications, but the acceptable process window may vary substantially.
For pipe extrusion, PVC SG5 is often chosen because its molecular-weight level can support rigid applications without becoming unnecessarily difficult to process in properly configured equipment. The final result still depends heavily on stabilizer selection, processing aid level, impact modification where required, filler treatment, lubrication balance, and die design. Resin is the foundation, not the complete formula.
Profile extrusion can be more sensitive to small shifts because the melt must fill detailed die geometry and retain shape through calibration. A compound that runs acceptably in a round pipe die may not give the same surface quality or dimensional control in a multi-cavity profile die. This is a reason to qualify resin performance in the actual product format rather than relying only on a general grade description.
For fittings, especially complex molded parts, the focus often shifts toward flow consistency and fusion quality in areas where melt fronts meet. A material that seems easy to fill is not automatically the preferred choice if it creates weak-looking weld regions or unstable shrinkage. Processing temperature and residence time deserve close attention because PVC can degrade when exposed to excessive heat history.
Do not use temperature as the first cure for every inconsistency
Increasing barrel or die temperatures is a common response when fusion seems incomplete. Sometimes that adjustment is appropriate, but it should follow evidence rather than guesswork. PVC has a limited thermal processing window, and additional heat can bring a separate risk: discoloration, odor, plate-out, loss of surface quality, or gradual degradation.
A more reliable sequence is to verify material condition, dry blend consistency, feed stability, screw condition, and actual temperature control before changing the setpoints. Check whether the displayed temperature matches the real zone condition, especially if sensors, heaters, or cooling systems may be drifting. Examine whether screen packs, adaptors, or die passages have accumulated deposits that increase pressure independently of resin behavior.
Lubricant changes also need restraint. Internal and external lubrication influence fusion timing and metal release in different ways. Adding more lubricant to solve high torque may reduce fusion; reducing lubricant to force fusion may increase sticking or thermal stress. The correct direction depends on the observed behavior and on the existing formulation, not on a universal rule.
Receiving and storage details that prevent avoidable variation
Even a correctly selected resin can become harder to process if receiving and storage practices are weak. Keep bags or bulk material protected from contamination, excessive moisture exposure, and mix-ups with other grades. Clearly separate resin lots until they are released for use under the site’s normal control process. If partial bags are returned to storage, identify them carefully rather than treating all white powder materials as interchangeable.
For facilities purchasing several chemical materials at once, segregation matters beyond PVC handling. Unrelated materials should remain clearly identified and stored according to their own handling requirements. For example, when sourcing ancillary chemicals such as Potassium iodide CAS#7681-11-0, it should not be introduced into PVC material areas or combined with resin inventory simply because it arrived in the same procurement shipment. One-stop purchasing can simplify ordering, but it does not replace material identification and storage discipline.
Before a new resin lot enters routine production, a short controlled trial is usually more useful than a full-scale immediate switch. Run enough material to observe feed behavior, torque or load pattern, pressure stability, surface condition, and dimensional response. Keep the rest of the formulation and operating conditions as stable as possible during the comparison. This makes the trial informative rather than anecdotal.
When a nominally similar resin should not be treated as a direct substitute
It is reasonable to compare products within the same suspension PVC family, but direct substitution should be approached carefully when the application has tight mechanical, appearance, or dimensional requirements. Differences in K-value range can be only part of the story. Particle porosity affects additive uptake, bulk density can affect feeding and mixing, and thermal stability behavior can influence the usable processing window.
A change may be manageable through formulation tuning, but that does not mean tuning is always necessary or desirable. If a production line is already operating near a narrow fusion or thermal limit, a resin that requires significant process changes may create more risk than value. In that situation, the better decision is often to retain a material with demonstrated consistency or perform a formal qualification trial before committing to a change.
A practical way to make the next decision
When pipes, profiles, or fittings show unexpected variation, begin with evidence rather than with a temperature increase. Confirm the resin identity and relevant technical data. Compare the current lot with a stable reference where possible. Review dry blend preparation and material storage. Watch pressure, torque, output, surface condition, and dimensional behavior as one connected process rather than as isolated readings.
PVC SG5 remains a useful grade for many rigid PVC applications because it sits in a practical molecular-weight range for common extrusion and molding work. Its K-value should be treated as a processing guide and a product-performance clue, not as a number to consider only during purchasing. Once that distinction is understood, material changes become easier to evaluate, troubleshooting becomes more disciplined, and unnecessary formulation changes are less likely to create a second problem while trying to solve the first.
Related Picks
 Butylated Hydroxytoluene Price Drivers: Supply, Purity, and Purchasing Risk FactorsOct 21, 2026Butylated Hydroxytoluene price trends depend on supply stability, purity, logistics, and purchasing risk. Learn how to compare quotes wisely and reduce sourcing costs.
 Sodium Tripolyphosphate Price Trends: Raw Material and Energy ExposureOct 20, 2026Explore sodium tripolyphosphate price trends, from phosphate and soda ash costs to energy exposure. Learn how to compare quotes, manage sourcing risks, and make smarter purchasing decisions.
 Acetonitrile Shipment to Vietnam Successfully Dispatched; RCEP Benefits Boost Fine Chemical Trade with ASEANSep 16, 2026A shipment of industrial-grade acetonitrile from our company has recently been loaded and dispatched following the completion of standardized hazardous material packaging and container securing procedures.
 Nigerian Client’s Order of 4 Containers of Vinyl Acetate Successfully Loaded and Shipped to West AfricaSep 16, 2026We recently completed the loading of a vinyl acetate order for a Nigerian client; four containers of the product have been successfully packed and are ready for shipment to Nigeria.




Question Consultation
Send Us Your Inquiry Today

Luxi Chemical is a professional chemical product supplier with ample stock of all chemical categories and excellent quality, welcome your purchase inquiry.

