


PVC Granules for Injection Molding: Color Control, Flow, and Impact Strength
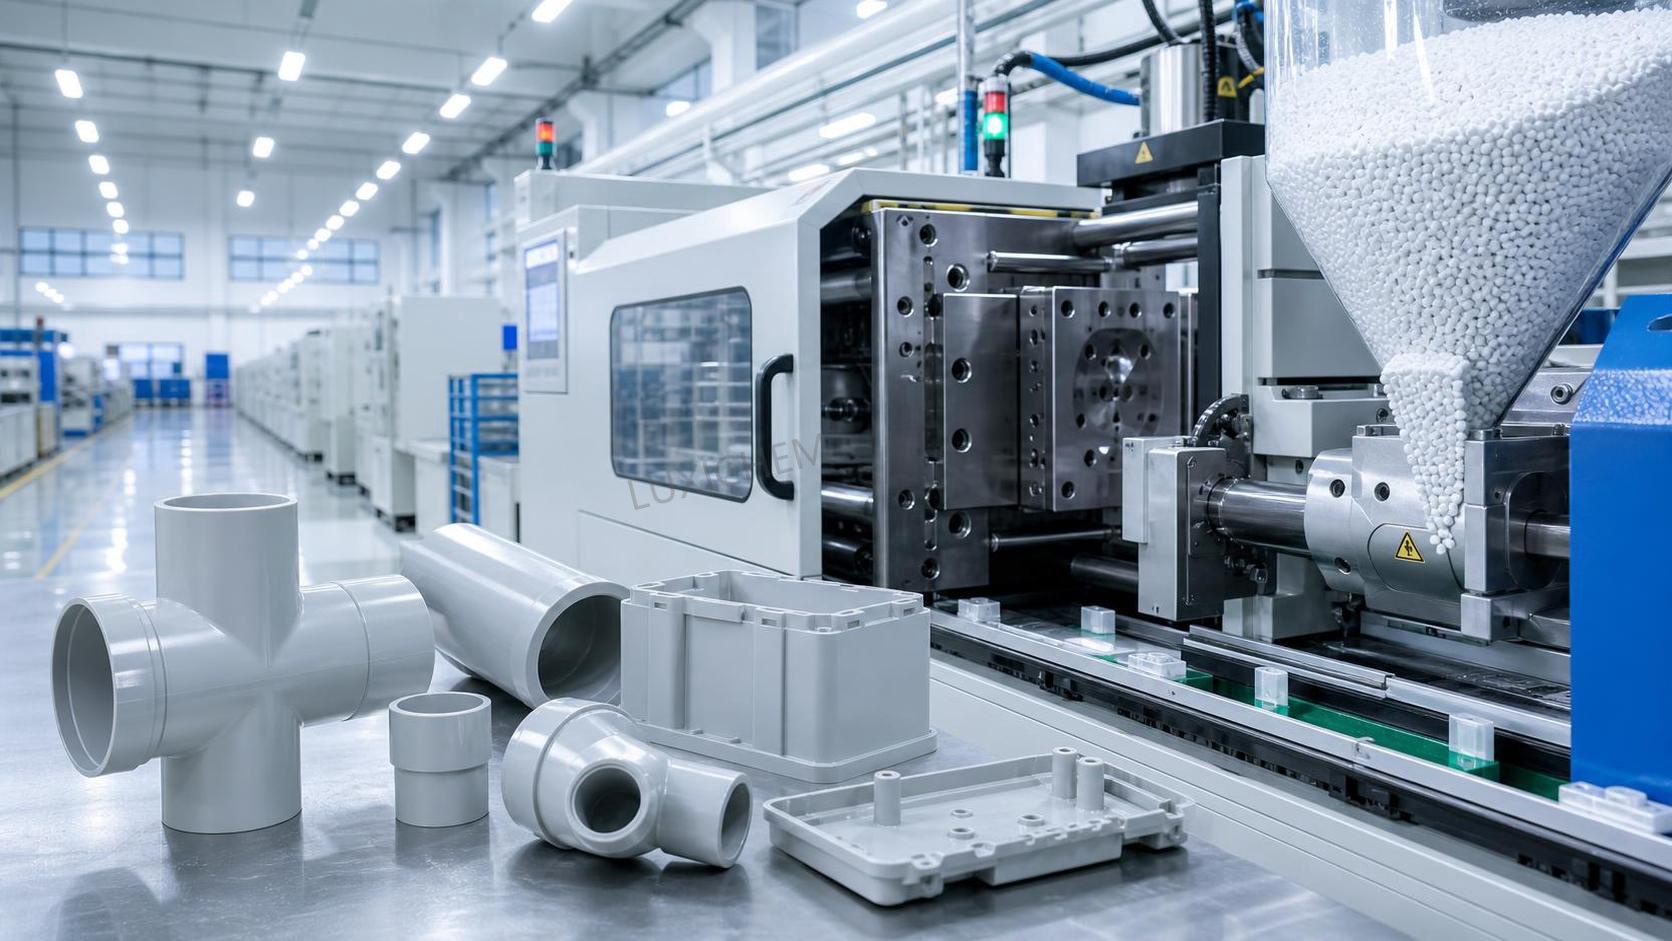
Injection-molded PVC parts are often judged by visible appearance first: a housing looks clean or streaky, a fitting matches the approved shade or does not, a handle feels robust or cracks when dropped. Yet those outcomes are determined well before the part reaches inspection. They begin with the formulation and consistency of the PVC granules, then depend on how that material responds to heat history, shear, mold filling, cooling, and handling on the production floor.
For rigid PVC injection molding, the practical target is not simply a material that melts. PVC does not behave like a broadly forgiving commodity resin. It must fuse within a controlled processing window without degrading, flow sufficiently to fill the cavity, retain enough melt strength to avoid unstable behavior, and deliver the required impact resistance after cooling. Color control, flow, and impact strength are therefore linked rather than separate purchasing specifications.
A batch can have an acceptable nominal color but create yellowing during molding. Another can show good flow in a standard test but fail in a thin rib, a long-flow fitting, or a multi-cavity tool. A high-impact formulation may resist breakage but bring a cycle-time penalty or reduce surface gloss. Effective material selection starts by connecting the granule specification to the actual part, mold, machine, and operating conditions.
Color stability is a processing issue, not only a color-matching issue
Color variation in PVC parts is commonly blamed on pigment dispersion, but the more difficult cases are caused by uneven thermal history. PVC is sensitive to excessive heat exposure. If melt temperature, residence time, barrel dead spots, or shear heating exceed the usable window, degradation can begin. Early signs include a cream or off-white shift in natural compounds, yellowing in light colors, loss of brightness in colored parts, dark streaks, and, in severe cases, black specks or a burnt odor.
The granule supplier’s color target should be assessed together with heat stability. A plaque made under controlled laboratory conditions may look acceptable, while production parts show a shift because the molding cycle is longer, the shot size is too small for the barrel, or the mold requires higher injection pressure. That is why color approval based only on loose granules or a single molded sample can be misleading.
For parts requiring repeatable shade, such as electrical accessories, pipe fittings, closures, furniture components, and visible appliance parts, a useful approval process includes molded reference plaques produced under agreed conditions. The reference should identify the mold or plaque geometry, processing temperature range, residence time, and lighting condition used for visual evaluation. Instrumental color measurement can help control batch-to-batch variation, but visual checks still matter because gloss, surface texture, and lighting can change how the same measured color is perceived.
On the machine, a gradual shift toward yellow usually deserves immediate investigation. Increasing barrel temperatures to solve a filling issue may temporarily improve flow while accelerating discoloration. The better response is to determine whether the restriction is caused by inadequate plasticization, low actual mold temperature, a cold gate, poor venting, excessive regrind, or a formulation that is too stiff for the part geometry.
Dark specks should not automatically be treated as a pigment defect. They can result from degraded PVC trapped in a nozzle, screw tip, non-return valve area, runner, or barrel corner. After a long stoppage, a purge and restart procedure is especially important. PVC should not be left at processing temperature without a clear operating plan, as extended residence raises the risk of degradation and corrosive decomposition products.
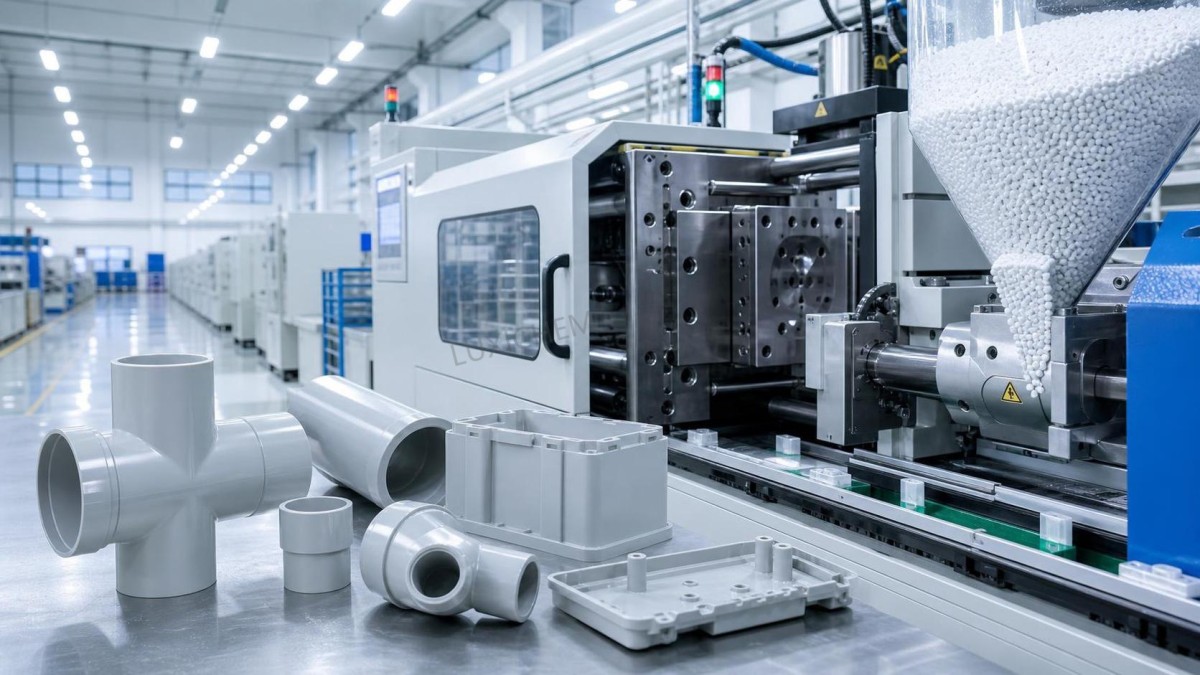
What “good flow” means in a PVC injection-molding application
Flow is often requested as a single number, but the practical question is whether the compound will fill the intended cavity consistently within a safe temperature and pressure range. The answer depends on part thickness, flow length, gate design, number of cavities, mold cooling balance, surface finish, and the injection unit itself.
Rigid PVC compounds are generally supplied as formulated granules containing PVC resin, stabilizer systems, lubricants, processing aids, fillers where applicable, pigments, and impact modifiers. These components determine how the material gels and flows under shear. A compound with higher apparent flow may support thin walls or long flow paths, but it may also be more sensitive to flash, sink behavior, weld-line appearance, or dimensional variation. A lower-flow compound may be suitable for thick-wall fittings but become difficult to process in detailed parts with narrow gates.
For day-to-day molding, stable flow is more valuable than an aggressively high flow rating. Stable flow means that a modest adjustment in barrel temperature or injection speed does not produce a disproportionate change in part weight, flash, short-shot risk, or color. This stability gives the processor a workable operating window and reduces dependence on constant machine correction.
Several symptoms help distinguish material-related flow limitations from machine or mold issues:
- Short shots at the same location may indicate a cold section of the mold, restricted venting, an undersized gate, or a compound unsuited to the required flow length.
- Inconsistent part weight often points to poor shot control, unstable cushioning, feed inconsistency, or variation in granule bulk behavior rather than resin flow alone.
- Flash appearing after temperature increases suggests that the process is being pushed to compensate for another restriction. Clamp force, parting-line condition, cavity pressure, and gate balance should be reviewed.
- Burn marks near the end of fill can result from trapped air and poor venting. Raising temperature may worsen the visual defect rather than solve it.
- High injection pressure with poor surface reproduction may indicate insufficient mold temperature, inadequate fusion, restricted runners, or excessive filler loading for the application.
Machine selection matters. Injection units that are oversized relative to the shot can create excessive residence time. Units that are too small may require operation near their limits, increasing shear and reducing process stability. Screw design, compression ratio, check-ring condition, and temperature-zone response all influence how PVC granules are plasticized. When changing suppliers or formulations, the initial trials should not begin at the highest available temperature. A controlled temperature profile, moderate back pressure, and documented changes provide more useful information than a fast attempt to force a complete fill.
Impact strength must be evaluated in the finished part
Impact resistance is often discussed as a material property, but molded-part performance is shaped by more than the granule formulation. Notches, sharp internal corners, weld lines, gate vestiges, knit lines around holes, residual stress, and low service temperature can all reduce real-world toughness. A compound that performs well in a standardized specimen may still fail at a vulnerable feature in a finished component.
Impact-modified PVC granules are commonly used where brittleness is unacceptable: tool housings, clips, utility boxes, furniture components, profiles converted through injection molding, protective covers, and fittings exposed to handling or installation loads. The required level of modification should reflect the expected service conditions rather than a general request for “high impact.” A part installed indoors at stable temperature faces a different risk profile from one exposed to cold outdoor handling, repeated assembly stress, or impact during transport.
There are trade-offs. Increasing impact modification can affect hardness, stiffness, heat resistance, gloss, flow behavior, and cost. Heavy filler use may support stiffness or cost objectives but can reduce impact performance if the formulation and dispersion are not appropriate. The correct choice is rarely the maximum impact value available. It is the formulation that meets the part’s failure-risk requirement while remaining stable in the chosen mold and cycle.
When evaluating a new grade, simple production-relevant checks can be more revealing than a datasheet comparison. Mold parts from the critical cavity positions. Test samples at the lowest anticipated service temperature if the application warrants it. Include weld-line regions and sections near holes or snap features. Compare not only catastrophic breakage but whitening, cracking, and permanent deformation. If a part is assembled with screws, inserts, or press fits, evaluate those operations after conditioning, not immediately after molding alone.
The formulation must suit the process route
Not all PVC granules marketed for molded goods are interchangeable. A compound developed for extrusion may not provide the fusion behavior, flow, or thermal response required in injection molding. Similarly, a formulation suitable for opaque industrial parts may not meet the appearance demands of a glossy consumer component. The requested application should be communicated in terms of geometry and processing conditions, not only as “PVC injection grade.”
A useful technical brief for a material trial includes the part weight, nominal and minimum wall thickness, longest flow length, gate type and gate thickness, number of cavities, target cycle time, desired surface appearance, color standard, expected service temperature, impact exposure, and any relevant regulatory restrictions. This information helps determine whether the priority should be easier flow, improved heat stability, higher impact resistance, lower gloss variation, or reduced plate-out tendency.
Catalog management also requires discipline in multi-product chemical supply chains. Product proximity in a catalog does not imply processing compatibility or application relevance. For example, Testosterone CAS#58-22-0 is a distinct chemical product and has no role in PVC injection-molding formulation or material substitution. Clear product identification, batch documentation, and segregated storage are basic safeguards against receiving and handling errors.
Receiving checks can prevent avoidable molding problems
Even a well-selected formulation can create trouble when handling conditions are inconsistent. Each delivery of PVC granules should be traceable to its batch documentation and checked against the approved grade, color, packaging condition, and quantity. Bags or bulk containers showing water exposure, tears, contamination, or unclear identification should be isolated before they reach the hopper.
PVC compounds do not usually present the same moisture sensitivity as some hygroscopic engineering plastics, but clean, dry storage remains important. Surface moisture and contamination can contribute to splay, surface marks, unstable feeding, or visual defects. Opened bags should be protected from dust, mixed materials, and accidental regrind contamination. Where drying is considered, it should follow the compound supplier’s guidance; unnecessary or excessive heating can create its own processing risks.
Regrind policy deserves particular attention. Clean, traceable runner regrind from the same grade and color may be usable within a controlled percentage, depending on the part and application. But regrind increases the material’s thermal history. In visible, high-impact, regulated, or close-tolerance parts, even small additions may affect color consistency, impact behavior, surface quality, or lot traceability. Mixed-color or unknown-origin regrind should not be used to solve a cost problem in a critical part.
Use a trial plan that separates formulation effects from process effects
A common mistake during material changes is to alter several settings at once. If barrel temperatures, injection speed, holding pressure, cooling time, mold temperature, and material grade are all changed during the same trial, it becomes impossible to identify why the result improved or deteriorated.
A more reliable approach starts with baseline machine conditions that have been proven on a comparable PVC grade. Record melt preparation settings, actual cycle time, cushion, peak injection pressure, holding profile, part weight, visual appearance, and key dimensions. Then evaluate the new PVC granules through a limited, planned adjustment sequence. Observe how the process window behaves rather than seeking one visually acceptable part.
The most useful signs of a suitable grade are repeatability over a normal production run, limited color drift after startup, stable part weight, acceptable pressure demand, clean release, and consistent impact performance in the part’s critical zones. A grade that produces excellent parts for ten cycles but begins to discolor, plate out, or fluctuate after extended running is not yet a validated solution.
For production teams, the practical value of well-matched PVC granules is fewer compromises. The material should not force repeated temperature escalation to fill the mold, excessive packing to control shrinkage, or broad acceptance of color variation to maintain output. When color stability, flow behavior, and impact strength are evaluated together, the result is a more predictable process and a part that remains fit for its intended service rather than merely acceptable at the end of the molding machine.
Related Picks
 Butylated Hydroxytoluene Price Drivers: Supply, Purity, and Purchasing Risk FactorsOct 21, 2026Butylated Hydroxytoluene price trends depend on supply stability, purity, logistics, and purchasing risk. Learn how to compare quotes wisely and reduce sourcing costs.
 Sodium Tripolyphosphate Price Trends: Raw Material and Energy ExposureOct 20, 2026Explore sodium tripolyphosphate price trends, from phosphate and soda ash costs to energy exposure. Learn how to compare quotes, manage sourcing risks, and make smarter purchasing decisions.
 Acetonitrile Shipment to Vietnam Successfully Dispatched; RCEP Benefits Boost Fine Chemical Trade with ASEANSep 16, 2026A shipment of industrial-grade acetonitrile from our company has recently been loaded and dispatched following the completion of standardized hazardous material packaging and container securing procedures.
 Nigerian Client’s Order of 4 Containers of Vinyl Acetate Successfully Loaded and Shipped to West AfricaSep 16, 2026We recently completed the loading of a vinyl acetate order for a Nigerian client; four containers of the product have been successfully packed and are ready for shipment to Nigeria.




Question Consultation
Send Us Your Inquiry Today

Luxi Chemical is a professional chemical product supplier with ample stock of all chemical categories and excellent quality, welcome your purchase inquiry.

